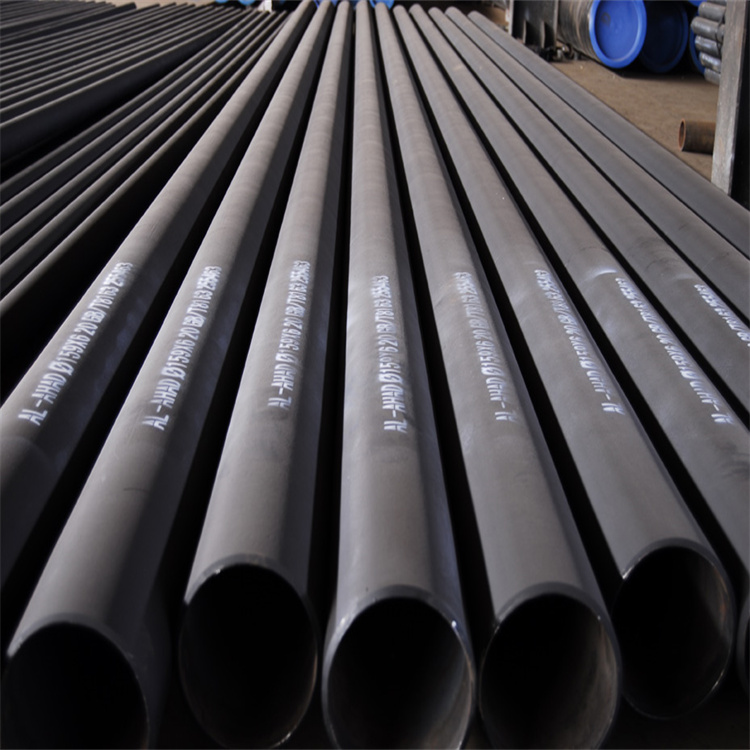
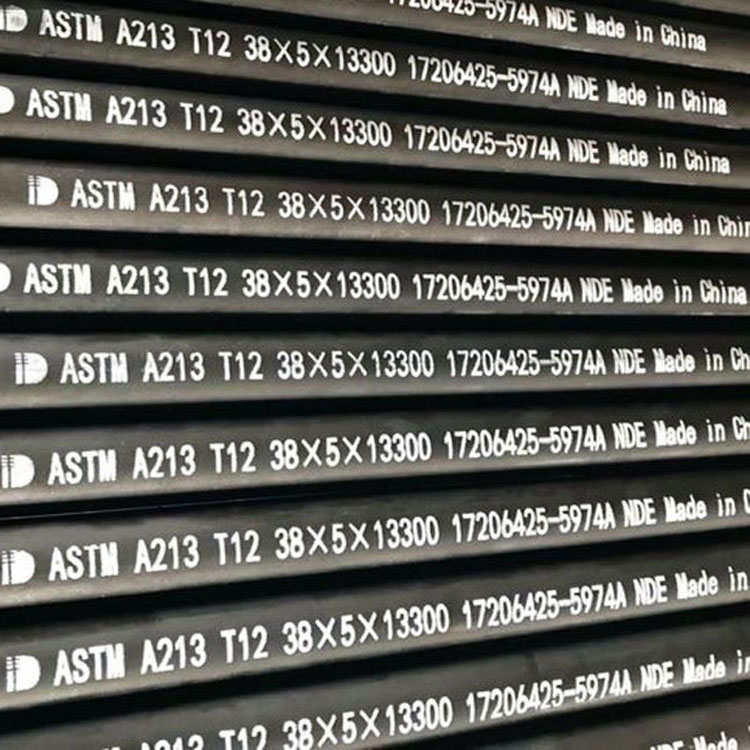
The full product name — cold drawn seamless precision hydraulic cylinder honed tubing — carries four distinct technical descriptors, and each one matters. “Cold drawn” describes the forming process. “Seamless” describes the tube construction. “Precision” describes the tolerance class. “Honed tubing” describes the bore finishing operation. Together they define a product that occupies a specific position in the steel tube supply chain: a ready-to-use cylinder barrel that has been engineered from raw billet to finished bore through a sequence of controlled operations, each of which improves the tube’s geometry, surface, or mechanical properties.
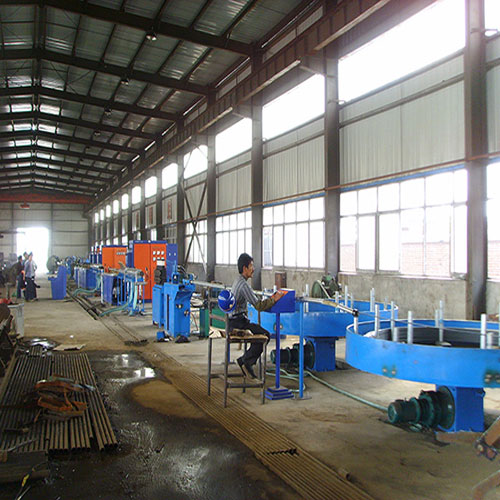
Cold drawing is a metal forming operation in which a tube blank is pulled through a precision die (controlling the outer diameter) over a hardened mandrel or plug (controlling the inner diameter and wall thickness) at room temperature. The process reduces the cross-section while simultaneously improving dimensional accuracy, surface finish, and mechanical properties.
Here is what happens at each stage:
The process starts with a hot-rolled seamless mother tube. Hot-rolled tube carries an oxide layer (mill scale) on its surfaces from the high-temperature forming operation. Before cold drawing, the tube is pickled in hydrochloric or sulfuric acid to remove this scale, then washed and coated with a phosphate or soap-based lubricant. The lubricant reduces friction during drawing and prevents galling — the transfer of steel particles from the tube to the die surface.
One end of the tube is swaged (pointed) to a smaller diameter so it can be gripped by the drawing jaw and fed through the die. A hydraulic or mechanical draw bench pulls the tube through the die and over the mandrel in a single pass. The reduction per pass typically ranges from 15% to 35% of the cross-sectional area, depending on the material grade and the starting dimensions. Multiple passes may be used with intermediate annealing to achieve large total reductions or very small final diameters.
After drawing, the tube is straightened (typically on a multi-roll rotary straightener), cut to length, and inspected. If the specified delivery condition requires stress relief, the tube is annealed at 540–560°C for 2–4 hours to reduce residual stresses without eliminating the strength gain from cold working. The tube may then proceed to honing or be shipped as cold-drawn precision tubing for the customer to hone in-house.
The critical distinction between cold drawing and hot rolling is temperature. In hot rolling, the steel is plastically deformed above its recrystallization temperature (approximately 1200°C for carbon steel), meaning the grains reform as they are shaped. In cold drawing, the steel is deformed below recrystallization temperature, so the grains are elongated and the dislocation density increases — a phenomenon called strain hardening or work hardening. This metallurgical change is what gives cold drawn tube its superior strength and dimensional stability.
The strength gain from cold drawing is not a surface effect — it is a through-wall metallurgical change. When steel is plastically deformed at room temperature, dislocations (linear defects in the crystal lattice) multiply and entangle. These dislocation tangles impede further deformation, which means more force is required to yield the material. The result is a measurable increase in yield and tensile strength.
The magnitude of this increase depends on the steel grade and the amount of cold reduction applied:
| Material Grade | Hot-Rolled Yield (MPa) | Cold Drawn Yield (MPa) | Strength Increase |
|---|---|---|---|
| ST52.3 / E355 | 355 (min) | 420–480 | 18–35% |
| SAE 1020 | 295 (min) | 360–420 | 22–42% |
| SAE 1045 | 310 (min) | 420–520 | 35–68% |
| 27SiMn | ~540 | 650–780 | 20–44% |
Values are approximate and depend on reduction ratio per pass and post-draw heat treatment. Stress-relieved (BK+S) condition retains approximately 80–90% of the as-drawn strength gain.
This strength increase has a direct implication for hydraulic cylinder barrel design: a cold drawn tube can achieve the same pressure rating as a hot-rolled tube with a thinner wall. For a 100 mm bore cylinder at 250 bar, the minimum wall in ST52 hot-rolled (355 MPa yield, safety factor 4) is approximately 14 mm. The same calculation using cold drawn ST52 (450 MPa yield) gives a minimum wall of approximately 11 mm — a 21% reduction in wall thickness and corresponding material savings. In practice, most cylinder manufacturers maintain the same wall for both, treating the strength increase as additional safety margin rather than as an opportunity to downsize.
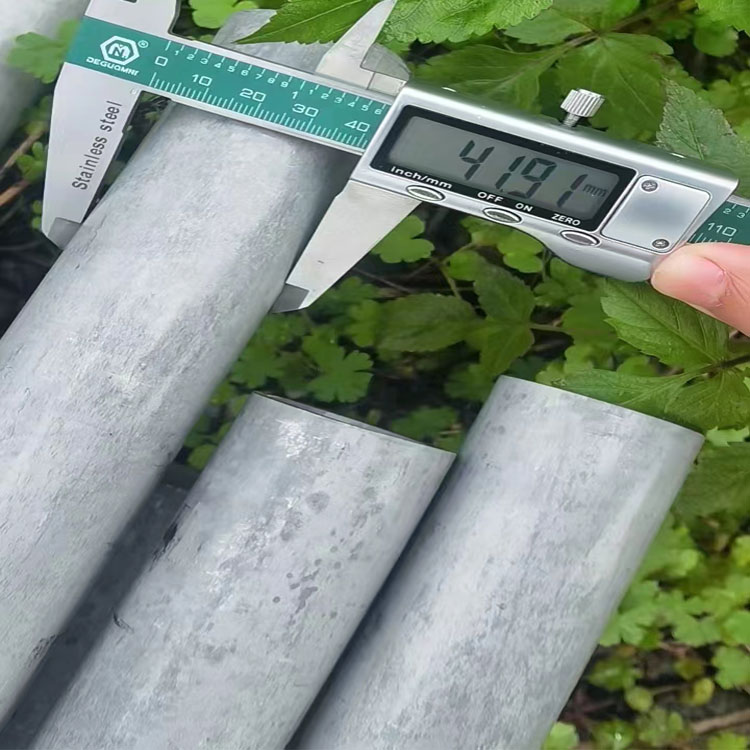
The most immediately measurable difference between cold drawn and hot-rolled seamless tube is dimensional accuracy. Hot rolling operates at temperatures where thermal expansion, scale formation, and die wear introduce variability. Cold drawing at room temperature, using hardened precision tooling, controls dimensions to a fraction of what hot rolling achieves.
| Parameter | Hot-Rolled Seamless | Cold Drawn Seamless | Improvement Factor |
|---|---|---|---|
| OD Tolerance | ±0.5–1.8 mm | ±0.05–0.10 mm | 10–18× tighter |
| ID Tolerance | ±0.5–2.0 mm | ±0.05–0.15 mm | 10–13× tighter |
| Wall Thickness Variation | ±10–15% of nominal | ±5% of nominal | 2–3× tighter |
| Outer Surface Ra | 3.2–12.5 μm (scaled) | 0.4–1.6 μm (bright) | 5–20× smoother |
| Inner Surface Ra | 6.3–12.5 μm | 0.8–3.2 μm | 4–10× smoother |
| Straightness | 1.0–2.0 mm/m | 0.3–0.5 mm/m | 3–4× straighter |
| Yield Strength (ST52) | 355 MPa | 420–480 MPa | 18–35% higher |
These differences compound when the tube enters the honing operation. A hot-rolled tube with ±1.5 mm OD variation and Ra 12.5 μm inner surface requires significant material removal during honing to reach H8 tolerance and Ra 0.4 μm — sometimes 0.5 mm or more of stock per side. A cold drawn tube starting at ±0.08 mm and Ra 1.6 μm needs only 0.05–0.15 mm of honing stock. The practical consequences are shorter honing cycle times, less abrasive consumption, and a bore with more uniform geometry because the honing stones remove less material and follow a more accurate starting surface.
Before a tube is cold drawn, it must exist as a hollow blank. There are three common methods for producing this blank, and the choice affects the finished honed tube’s pressure-bearing consistency.
A seamless tube is produced by piercing a solid round steel billet on a rotary piercing mill. The billet is heated to forging temperature and forced over a mandrel by angled rolls that both rotate and advance the billet, creating a hollow shell with no longitudinal seam. The shell is then rolled or drawn to final dimensions.
The defining property of seamless tube is circumferential uniformity. With no weld seam, the wall thickness, microstructure, and mechanical properties are consistent around the entire circumference. There is no heat-affected zone, no weld reinforcement to remove, and no risk of weld-line defects propagating under cyclic pressure. For a hydraulic cylinder barrel that must contain 250–350 bar of pulsating hydraulic fluid, this uniformity is the primary reason seamless tube is specified.
ERW tube is formed by rolling a flat steel strip into a cylindrical shape and welding the longitudinal edges using electric resistance. The weld creates a heat-affected zone with different grain structure from the parent metal, and the weld bead — even after scarfing (trimming) — leaves a microstructural discontinuity. ERW tube is less expensive than seamless but is not the standard for hydraulic cylinder service because the weld seam can become a failure initiation point under high cyclic pressure.
DOM tube bridges the gap between ERW and seamless. It starts as ERW tube, then is cold drawn over a mandrel. The drawing operation cold-works the entire tube — including the weld zone — to the point where the weld seam becomes nearly invisible in cross-section. DOM tube achieves dimensional accuracy comparable to cold drawn seamless and is used in medium-pressure hydraulic cylinders (100–200 bar). It costs 15–25% less than seamless because the raw ERW blank is cheaper than a pierced billet.
However, DOM tube retains a microstructural discontinuity at the former weld location. Even though the weld is visually indistinguishable after drawing, the heat-affected zone has a different grain size and hardness from the parent metal. Under cyclic loading, this difference can lead to preferential fatigue crack initiation at the weld line. For this reason, most cylinder specifications for pressures above 250 bar explicitly require seamless construction.
| Property | Cold Drawn Seamless | DOM | ERW (not cold drawn) |
|---|---|---|---|
| Weld seam | None | Present (nearly invisible after drawing) | Present (visible) |
| Wall uniformity | Best (circumferentially uniform) | Good (slight variation at weld zone) | Moderate |
| Pressure rating | Highest (no weak point) | Good for medium pressure | Lower; seam limits pressure |
| Typical pressure service | 250 bar and above | 100–200 bar | Below 100 bar or non-pressure |
| Cost relative to seamless | Baseline | 15–25% lower | 30–40% lower |
| Fatigue life | Longest (no discontinuity) | Moderate (weld zone as initiation point) | Shortest |
Cold drawn precision seamless tubes are supplied in several delivery conditions defined by DIN 2391 and EN 10305-1. The delivery condition describes the post-drawing heat treatment and determines the balance between strength, ductility, and dimensional stability. Selecting the right condition for hydraulic cylinder honed tubing affects both the honing operation and the subsequent barrel welding process.
| Condition Code | Name | Heat Treatment | Yield Strength (ST52) | Elongation | Best For |
|---|---|---|---|---|---|
| BK | Cold drawn, hard | None (as-drawn) | ~480 MPa | 8–12% | Maximum strength; non-welded applications |
| BK+S | Cold drawn, stress-relieved | 540–560°C, 2–4 hrs | ~430–450 MPa | 12–16% | Welded cylinder barrels (most common) |
| C | Cold drawn, soft | Full anneal | ~355 MPa | 20–24% | Forming or bending operations |
| N | Normalized | Above AC3, air-cooled | ~355 MPa | 22–25% | Impact resistance, low-temperature service |
Approximate values for ST52.3 / E355 grade. Actual values per heat lot are documented on the EN 10204 3.1 certificate.
BK+S (stress-relieved) is the most commonly specified delivery condition for hydraulic cylinder honed tubing, and for good reason. After cold drawing, the tube carries residual stresses from the non-uniform plastic deformation across the wall. When the tube is later welded to end caps, these residual stresses superimpose with welding thermal stresses and can distort the bore. Stress-relieving at 540–560°C — below the recrystallization temperature — reduces residual stress by approximately 80–90% while retaining most of the strength gain from cold working. The result is a tube that is strong enough for high-pressure service and dimensionally stable during barrel welding.
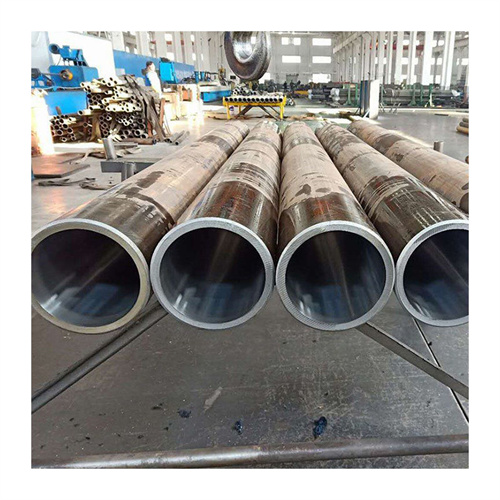
The honing operation — abrasive finishing of the bore to final dimensions and surface specification — is the last manufacturing step before the tube becomes a cylinder barrel. The quality of the honed bore depends significantly on the quality of the tube entering the honing machine. Cold drawn seamless precision tube is the preferred starting material for honing for several specific, measurable reasons:
A cold drawn tube enters honing with an ID tolerance of ±0.05–0.15 mm and an inner surface Ra of 0.8–3.2 μm. To reach H8 tolerance (±0.04–0.06 mm) and Ra 0.2–0.4 μm, the honing operation removes only 0.05–0.15 mm of material per side. A hot-rolled tube entering honing with ±0.5–2.0 mm ID variation and Ra 6.3–12.5 μm requires 0.3–0.5 mm of material removal — three to five times more. Less removal means faster honing cycles, less abrasive stone wear, lower per-part cost, and a bore that more closely follows the cold drawn geometry.
Honing corrects geometry — but only within limits. If the starting tube has 0.5 mm of ovality or taper, honing may not fully correct it without removing so much material that wall thickness drops below specification. Cold drawn tube, with its tight starting geometry, enters honing with minimal ovality and taper. The honing stones refine an already-accurate bore rather than trying to fix a poor one, producing a more uniform cylindrical surface along the full length.
The cross-hatch pattern from honing is more consistent when the starting surface is smooth. A rough hot-rolled inner surface forces the honing stones to remove large peaks before establishing the cross-hatch, which can leave deep valleys that remain below the target Ra. Cold drawn tube starts with a surface that the honing stones can quickly bring to a uniform cross-hatch at the target Ra value.
The strain hardening from cold drawing remains in the finished honed tube (particularly in BK+S condition). This means the barrel benefits from higher yield strength than a hot-rolled-and-honed tube of the same grade, providing additional pressure-bearing margin or the option to reduce wall thickness for weight savings.
Seamless tube produced from a pierced billet has a homogeneous microstructure with no weld-line discontinuities. When ultrasonic testing (UT) is performed on the finished honed tube — increasingly required by OEM cylinder specifications for pressures above 150 bar — the absence of a weld seam eliminates the most common source of UT indications that would otherwise require investigation or rejection.
Cold drawn seamless precision tubing for hydraulic cylinder applications is governed by a family of national and international standards. These define chemical composition limits, mechanical property minimums, dimensional tolerance classes, delivery conditions, and inspection requirements:
| Standard | Title | Scope | Common Grades |
|---|---|---|---|
| DIN 2391 | Seamless Precision Steel Tubes | German standard for cold drawn precision seamless tube; defines dimensions, tolerances, delivery conditions | St37.4, St44.4, St52.3 |
| EN 10305-1 | Precision Steel Tubes — Part 1: Seamless Cold Drawn | European standard superseding portions of DIN 2391; defines technical delivery conditions | E235, E355 |
| ASTM A519 | Seamless Carbon and Alloy Steel Mechanical Tubing | American standard for seamless mechanical tubing including cold drawn grades | 1020, 1026, 1045, 4140 |
| JIS G3445 | Carbon Steel Tubes for Machine Structural Use | Japanese standard for precision mechanical tubing | STKM11A, STKM13C |
| GB/T 3639 | Seamless Cold-Drawn or Cold-Rolled Steel Tubes for Precision Applications | Chinese standard for precision seamless tubing | 20#, 45#, 27SiMn |
Every shipment of cold drawn seamless precision honed tubing should be accompanied by an EN 10204 3.1 mill test certificate documenting the chemical composition and mechanical properties of the specific heat lot. The 3.1 certificate is signed by the manufacturer’s authorized representative and is traceable to the heat number stamped or marked on the tube. This certificate is not optional for hydraulic cylinder barrel production — it is the buyer’s evidence that the material in the tube matches the specification on the drawing. Without it, the tube cannot be accepted into safety-critical cylinder production.
Cold drawn seamless precision honed tubing is produced across a range that covers most hydraulic cylinder bore sizes. The practical limits of cold drawing — die size, draw bench length, and reduction per pass — set the boundaries:
| Dimension | Typical Range | Notes |
|---|---|---|
| Inner Diameter (post-honing) | 20–400 mm | Below 20 mm: honing becomes impractical; above 400 mm: cold drawing limited by die availability |
| Outer Diameter | 32–480 mm | Larger ODs available from hot-rolled + honing route |
| Wall Thickness | 2.5–40 mm | Very thin walls (< 2 mm) require specialized drawing; very thick walls use hot-rolled parent |
| Standard Length | 3–8 m (random) | Up to 12 m available; honing length limited by honing machine stroke |
| Typical Tolerance (ID, post-honing) | H7–H9 (ISO 286) | H8 standard; H7 for precision; H9 for pneumatic |
| Surface Roughness (Ra, post-honing) | 0.2–0.4 μm | Cross-hatch at 45° ± 5° for oil retention |
For bore sizes above 400 mm or wall thicknesses above 40 mm, cold drawing becomes impractical due to the force required to pull such a large section through a die. In these cases, the honed tube is produced from a hot-rolled seamless parent that is bored and then honed. The resulting product has looser starting tolerances but the honing operation brings the bore to the same final specification. Large-bore hydraulic cylinders (mining, offshore, steel mill) often use this route.
Cold drawn seamless precision hydraulic cylinder honed tubing is a product defined by a sequence of manufacturing decisions: seamless construction for circumferential uniformity, cold drawing for dimensional accuracy and strain-hardened strength, precision tolerance classes for consistent bore geometry, and honing for the surface finish and cross-hatch oil retention that hydraulic cylinder seals require. Each step in this sequence builds on the previous one — a cold drawn tube gives the honing operation a better starting surface, which produces a better bore, which gives the cylinder a longer seal life and higher pressure rating.
When sourcing this product, the specification should address all four attributes in the product name: “seamless” (no weld seam), “cold drawn” (BK+S delivery condition for welded barrels), “precision” (H7–H8 tolerance per DIN 2391 / EN 10305-1), and “honed” (Ra 0.2–0.4 μm with cross-hatch). A tube that meets only some of these criteria — for example, a DOM tube sold as “seamless,” or a hot-rolled tube honed to H8 but without the strength gain from cold drawing — may look similar on paper but will not perform the same in a hydraulic cylinder under pressure. The full product name exists because every word in it represents a manufacturing choice that affects the finished barrel’s performance.
Cold drawn seamless precision hydraulic cylinder honed tubing is a steel tube produced by cold drawing a seamless (weld-free) parent tube through a die and over a mandrel at ambient temperature, then honing the inner bore to final dimensions. The cold drawing process tightens tolerances to ±0.05–0.10 mm, improves surface finish to Ra 0.4–1.6 μm, and raises yield strength by 20–40% through strain hardening. The subsequent honing operation brings the bore to H7–H9 tolerance and Ra 0.2–0.4 μm for hydraulic cylinder service.
Cold drawn seamless tube offers 5–10× tighter dimensional tolerances than hot-rolled tube (±0.05–0.10 mm vs ±0.5–1.8 mm), smoother surface (Ra 0.4–1.6 μm vs Ra 3.2–12.5 μm), and 20–40% higher yield strength from strain hardening. These properties mean less material removal during honing, shorter honing cycle times, more uniform bore geometry, and better pressure-bearing capacity in the finished cylinder barrel.
Cold drawn seamless tube is produced from a solid billet with no weld seam, offering circumferentially uniform wall thickness and the highest pressure consistency. DOM (Drawn Over Mandrel) tube starts as electric-resistance-welded tube that is cold drawn over a mandrel, making the weld seam nearly invisible. DOM delivers near-seamless dimensional performance at lower cost but retains a microstructural discontinuity at the weld. Seamless is specified for pressures above 250 bar; DOM is common at 100–200 bar.
Per EN 10305-1 and DIN 2391, delivery conditions include: BK (cold drawn, hard — maximum strain hardening, highest strength, lowest ductility), BK+S (cold drawn and stress-relieved — balanced strength and ductility, preferred for welded cylinder barrels), C (cold drawn, soft — annealed after drawing for maximum formability), and N (normalized — recrystallized grain structure for impact resistance). BK+S is the most common condition for hydraulic cylinder honed tubing.
Cold drawing raises yield strength by 20–40% compared to the hot-rolled parent material through strain hardening. For example, ST52 steel with a nominal yield of 355 MPa in the hot-rolled condition typically reaches 420–480 MPa after cold drawing. This increase comes from dislocation density multiplication and grain elongation. Stress-relieving at 540–560°C (BK+S condition) recovers some ductility while retaining approximately 80–90% of the strength gain.
The primary standards are DIN 2391 (German precision seamless steel tubes), EN 10305-1 (European seamless cold drawn precision tubes), ASTM A519 (American seamless carbon and alloy mechanical tubing), and JIS G3445 (Japanese carbon steel tubes for machine structural use). These standards define chemical composition, mechanical properties, tolerance classes, delivery conditions, and inspection requirements. EN 10204 3.1 mill test certificates provide material traceability for each heat lot.
BK+S (cold drawn, stress-relieved) reduces residual stresses from the cold drawing operation by 80–90% through annealing at 540–560°C. This dimensional stability is critical when the tube is later welded to end caps — residual stresses from as-drawn (BK) condition combined with welding thermal stress can distort the bore by 0.05–0.15 mm near the weld zone. BK+S retains approximately 80–90% of the strength gain while preventing this distortion.